Views: 0 Author: Site Editor Publish Time: 2026-09-09 Origin: Site

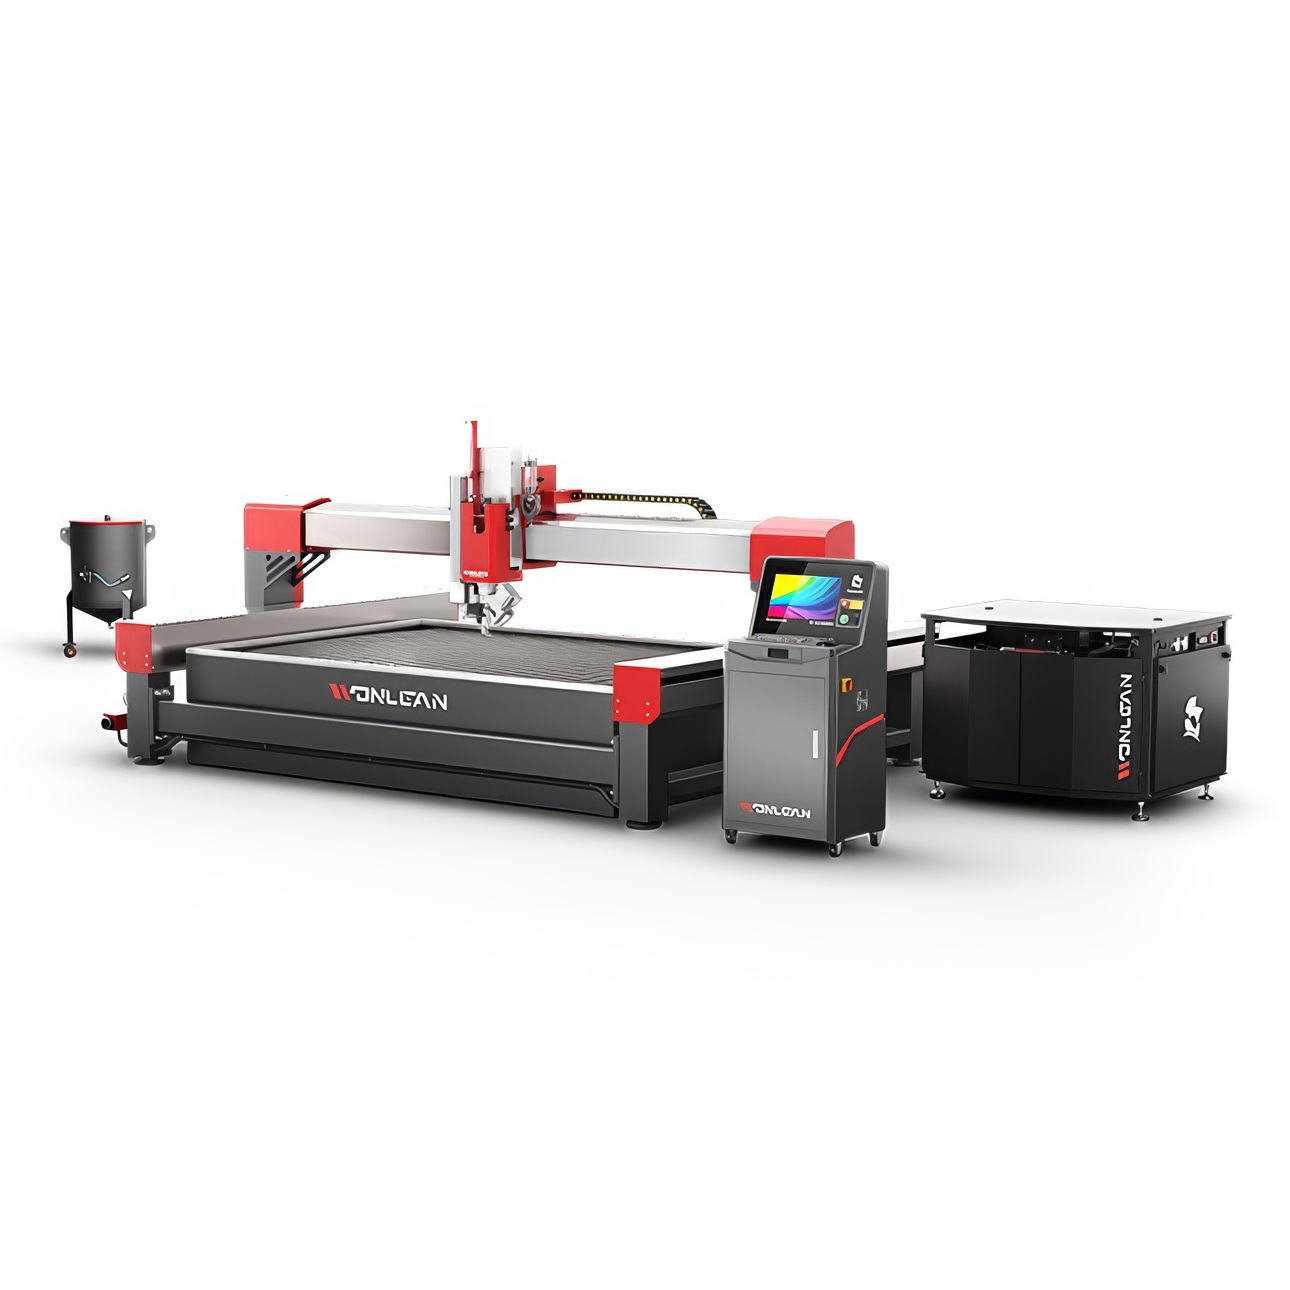
Metal fabrication demands precision. Thermal cutting methods like plasma and laser often induce material warping, edge hardening, and unwanted metallurgical changes. These thermal distortions compromise the structural integrity of aerospace-grade alloys and temperature-sensitive metals. To eliminate the Heat-Affected Zone (HAZ), fabricators are upgrading their equipment. You face a complex decision matrix when comparing systems. You must balance edge quality, material versatility, and long-term operational efficiency. Selecting the right waterjet cutting machine requires a deep understanding of pump mechanics, motion control capabilities, and facility infrastructure.
This guide provides an evidence-based framework for evaluating and selecting industrial waterjet systems. We examine how pump technology, software integration, production volume, and operator experience influence machine performance. You will learn how to match system architecture to specific fabrication requirements, ensuring consistent precision across materials ranging from thick steel to brittle ceramics.
HAZ Elimination: Abrasive waterjets cut via accelerated erosion, preserving the structural integrity of aerospace-grade alloys, thick steel, and temperature-sensitive metals without hardening the edges.
Pump Technology Dictates Operating Expenses: The choice between Direct Drive and Intensifier pumps directly impacts maintenance intervals, energy efficiency, and hourly operating costs.
Software is the Differentiator: Advanced control systems and taper-compensation software are critical for achieving tight tolerances (e.g., 0.015” accuracy) and minimizing kerf width.
Premium vs. Value Tier ROI: While buyers often seek "better for cheaper" alternatives, the upfront savings of entry-level machines must be weighed against the long-term reliability, parts availability, and community consensus surrounding established brands like OMAX and Flow.
Hidden Implementation Costs: Facility requirements—specifically water treatment, abrasive sludge disposal, and specialized plumbing—must be factored into the initial capital expenditure.
Establishing baseline expectations for a CNC waterjet cutting system for metal fabrication begins with understanding the trade-offs between cutting speed and edge quality. Waterjet edge finishes are universally categorized from Q1 to Q5. A Q1 finish represents a fast separation cut. It leaves noticeable striations and a rough texture suitable for scrap or parts requiring heavy post-processing. A Q5 finish delivers a highly precise, smooth edge with minimal taper. It operates at significantly slower feed rates. Operators must dial in these parameters based on the specific tolerance requirements of each part. High-density metals like Inconel or titanium require careful balancing of abrasive flow rates and pump pressure. This maintains a Q3 or Q4 finish without sacrificing excessive machine time.
Edge Quality Standard | Surface Finish Characteristics | Typical Application | Relative Cutting Speed |
|---|---|---|---|
Q1 (Separation) | Rough, heavy striations, visible drag lines | Scrap processing, rough blanks | Fastest (100%) |
Q2 (Rough) | Moderate striations, slight taper | Parts requiring secondary machining | Fast (80%) |
Q3 (Standard) | Smooth top half, slight striations at bottom | General fabrication, weldments | Medium (60%) |
Q4 (Good) | Very smooth, minimal visible striations | Precision parts, visible edges | Slow (40%) |
Q5 (Excellent) | Mirror-like finish, near-zero taper | Aerospace components, medical devices | Slowest (20%) |
Material versatility stands out as a primary operational advantage. A properly configured system handles varying thicknesses without requiring tooling changes. Operators can transition from cutting half-inch aluminum sheet to ten-inch thick carbon steel blocks using the same cutting head and abrasive mixture. This flexibility eliminates the setup downtime typically associated with swapping mechanical cutting tools or adjusting laser focal lengths. The stream pierces directly through thick materials. Operators must utilize specialized low-pressure piercing techniques for brittle or laminated materials. This prevents delamination or surface cracking during the initial penetration phase.
The reduction of secondary operations heavily influences the overall value of the machine. Thermal cutting methods like plasma leave hardened edges and heavy dross. These artifacts require extensive grinding, milling, or tapping before the part moves to assembly. Waterjet cutting produces clean, burr-free edges. The absence of a Heat-Affected Zone means the metallurgical structure of the edge remains identical to the parent material. Machinists can tap holes or perform secondary milling directly on the cut edge. They won't burn through expensive carbide tooling. Eliminating these secondary finishing processes streamlines the production workflow and increases daily throughput.
Workholding and fixturing present unique challenges in this environment. The cutting process generates significant multidirectional forces. These include hydrodynamic pushback and abrasive splashback. Parts must be secured firmly to the cutting bed slats to prevent shifting under the high-pressure stream. Underwater cutting dynamics also play a role. Submerging the material reduces noise and contains abrasive dust. However, it obscures the operator's view of the cutting action. When cutting thin sheet metal, the hydrodynamic pushback from the catcher tank water can lift the material off the slats. Operators place heavy lead weights on the sheet edges to keep it flat. If a part tips up after being cut, the rapid traverse of the cutting head can collide with it. This collision often shatters the brittle sapphire orifice or snaps the expensive mixing tube. Strategic placement of lead-ins and lead-outs ensures the scrap falls away safely.
The pump serves as the power plant of any waterjet system. It generates the ultra-high pressure required to accelerate the abrasive stream. The industry relies on two primary pump architectures: intensifier pumps and direct-drive pumps. Intensifier pumps utilize hydraulic pressure to drive a large piston. This piston pushes a smaller ceramic plunger into a water cylinder. This mechanical advantage generates pressures up to 90,000 PSI. Intensifiers excel in continuous, heavy-duty cycles. They easily support multiple cutting heads simultaneously. They provide a smooth, consistent pressure curve. An accumulator acts as a shock absorber to minimize pressure fluctuations during the stroke reversal.
Hydraulic intensifiers generate immense heat. They require dedicated cooling systems, typically a water-to-oil heat exchanger or a standalone chiller, to keep the hydraulic fluid within operating temperatures. If the fluid overheats, it degrades the hydraulic seals and causes erratic pump strokes. Changing the high-pressure seals on an intensifier involves depressurizing the system, unbolting the end bells, and carefully extracting the ceramic plungers. Operators must maintain absolute cleanliness during this process. Even a single grain of garnet entering the high-pressure cylinder will score the plunger and destroy the new seals instantly.
Direct-drive pumps operate differently. They utilize a crankshaft-driven mechanism similar to an automobile engine. An electric motor turns a crankshaft that drives three or more plungers directly into the water cylinders. This design eliminates the hydraulic system entirely. Direct-drive pumps offer significantly higher energy efficiency. They convert up to 85% of the electrical input into cutting power, compared to the roughly 65% efficiency of hydraulic intensifiers. However, they operate at slightly lower maximum pressures, typically capping around 60,000 PSI. The maintenance profiles also differ. Direct-drive pumps require more frequent, albeit simpler, seal replacements. Intensifier pumps run longer between rebuilds but demand more complex maintenance procedures involving hydraulic fluid management.
Cutting head configurations dictate the machine's material capabilities. Pure water cutting heads utilize a tiny jewel orifice. This is usually diamond, sapphire, or ruby. It creates a hair-thin stream of water. This configuration cuts soft materials like foam, rubber, gasket material, and thin plastics. Abrasive waterjet cutting introduces a mixing chamber below the jewel orifice. The high-velocity water stream creates a Venturi effect. It pulls abrasive garnet from a hopper into the mixing chamber. The water and garnet mix, accelerating down a tungsten carbide mixing tube. This abrasive stream erodes hard materials like metals, stone, and composites. The alignment of the orifice, mixing chamber, and mixing tube must remain perfectly concentric. This prevents premature wear and ensures optimal cutting performance.
Motion control and axis capabilities determine the geometric complexity the machine can achieve. Standard 3-axis systems move the cutting head along the X and Y axes over a flat bed. The Z-axis controls the height of the nozzle. These systems handle the vast majority of flat sheet metal fabrication. Advanced 5-axis systems introduce tilt and rotation capabilities to the cutting head. This articulation allows the machine to cut complex 3D parts. It performs weld preparations and executes precise bevels. 5-axis kinematics require highly sophisticated software. The software calculates the complex toolpaths and maintains the correct standoff distance as the head tilts across uneven surfaces.
Cutting accuracy relies heavily on taper control. A waterjet stream naturally loses energy as it penetrates material. This results in a V-shaped kerf where the bottom of the cut is narrower than the top. Dynamic cutting heads and predictive software compensate for this natural taper. The software calculates the exact amount of stream lag and taper based on the material type, thickness, and cutting speed. It then slightly tilts the cutting head. This is often just a fraction of a degree. It pushes the taper into the scrap side of the material. This active compensation maintains strict dimensional tolerances. It produces perfectly square edges on the finished part, even in thick materials.
Software integration dictates the daily usability of the machine. Proprietary software suites provide highly optimized cutting models. These are developed through decades of empirical testing. These platforms automatically adjust feed rates for corners, tight radii, and piercing routines. Modern CAM software handles the complex mathematics of kerf compensation automatically. The kerf is the width of the material removed by the stream, typically around 0.030 to 0.040 inches. The software offsets the toolpath by half the kerf width so the final part matches the exact dimensions of the CAD model. Advanced nesting algorithms analyze the geometry of multiple parts and arrange them on the sheet to minimize scrap. Good nesting software also sequences the cuts to maintain sheet stability. It cuts the inner holes first before cutting the outer perimeter, ensuring the part remains firmly attached to the heavy parent sheet during the delicate internal operations.
Operator experience and community consensus provide valuable insights into real-world machine performance. Machinists prioritize machine reliability and the ease of daily maintenance. Systems designed with accessible high-pressure plumbing, quick-change cutting heads, and straightforward abrasive delivery systems reduce daily downtime. The learning curve for new operators depends largely on the intuitiveness of the control interface. Machines with robust onboard diagnostics and clear error reporting empower operators. They can troubleshoot minor issues without calling for external service technicians. Engaging with user communities and reading field reports reveals the true operational characteristics of different brands.
Cross-material capabilities expand the utility of the machine across different manufacturing sectors. By adjusting pump pressure, piercing methods, and abrasive flow rates, a metal fabrication shop can transition to cutting brittle materials. For example, utilizing the machine as an industrial waterjet cutting system for ceramic cutting requires specific parameter changes. Operators must utilize low-pressure piercing. This prevents the initial water blast from shattering the ceramic tile or composite panel. Once the stream penetrates the material, the software ramps up the pressure to full cutting speed. This flexibility allows fabricators to diversify their service offerings. They do not need to invest in separate, specialized machinery for glass, stone, or advanced composites.
Evaluating premium versus value-tier systems requires looking past the initial machine specifications. Buyers often face the dilemma of choosing between established industry leaders and lower-tier imports. Premium brands invest heavily in proprietary pump technologies, advanced taper-compensation software, and robust motion control systems. These investments translate directly into higher machine uptime, tighter cutting tolerances, and longer intervals between maintenance cycles. Value-tier machines may offer similar static specifications on paper. However, they often utilize generic control software and off-the-shelf pump components. The long-term reliability, availability of proprietary replacement parts, and access to experienced service technicians heavily favor established manufacturers.
Consumables tracking forms a major part of operational management. Abrasive garnet represents the largest ongoing consumable demand. An aggressive cutting setup can consume one to two pounds of garnet per minute. Operators must balance the abrasive feed rate against the cutting speed. This optimizes performance without wasting garnet. Water consumption and electricity draw also factor into the daily operational footprint. The cutting head itself contains wear parts that require regular replacement. The jewel orifice and the tungsten carbide mixing tube degrade over time. This is due to the extreme velocity and abrasive friction. Tracking the lifespan of these components helps operators anticipate maintenance needs. It prevents sudden cut quality degradation.
Energy consumption varies significantly based on pump architecture. High-horsepower intensifier pumps draw substantial electrical current. This is especially true when operating at 90,000 PSI. The hydraulic system requires continuous power to maintain pressure, even during short pauses in the cutting program. Direct-drive alternatives draw less power overall and offer greater electrical efficiency. Evaluating the electrical draw over a standard annual shift schedule provides a clear picture of the machine's energy footprint. Facilities must ensure their electrical infrastructure can handle the peak amperage requirements of the pump motor. This is critical during startup sequences.
Comparing plasma, laser, and waterjet technologies highlights the specific performance niche of each method. Plasma cutting offers high speed for thick steel. However, it produces a massive Heat-Affected Zone, poor edge quality, and significant dross. Fiber lasers excel at high-speed cutting of thin-gauge sheet metal with excellent precision. They struggle with highly reflective materials like copper or brass. They lose efficiency on steel thicker than one inch. Waterjet cutting operates at slower feed rates than laser or plasma. It cuts virtually any material, regardless of thickness or reflectivity, without generating heat. When the application demands thick material processing, zero thermal distortion, and elimination of secondary finishing, the waterjet provides the most effective performance.
Facility preparation demands careful planning before the machine arrives. The physical infrastructure must support the immense weight of the equipment. A large waterjet catcher tank, filled with water, steel slats, and accumulated garnet sludge, weighs tens of thousands of pounds. Facilities often require reinforced concrete foundations. This prevents the machine from settling or shifting out of level over time. Specialized electrical drops must be installed to handle the high-amperage draw of the pump motors.
The abrasive delivery system relies on gravity and compressed air. A bulk hopper sits next to the machine and pushes garnet through a plastic tube to a smaller mini-hopper mounted on the Z-axis carriage. Moisture is the enemy of this system. If humidity enters the compressed air lines, the garnet clumps together and clogs the delivery tube. A clogged tube starves the cutting head of abrasive. The machine will continue moving, but the pure water stream will only score the surface of the metal, ruining the workpiece. Operators must install high-quality air dryers and moisture traps on the compressor lines to prevent these blockages.
Water quality directly impacts the lifespan of high-pressure pump components. Municipal water supplies contain dissolved solids, minerals, and silica. These act as microscopic abrasives inside the pump. Hard water causes calcium scaling on check valves and plungers. This leads to premature seal failure. Facilities must test their water quality and install appropriate treatment systems. Water softeners remove calcium and magnesium. Reverse osmosis (RO) systems strip out total dissolved solids (TDS). Chillers may also be necessary to regulate the inlet water temperature. Warm water degrades high-pressure seals much faster than cold water.
Abrasive removal and waste management require dedicated logistical planning. The cutting process generates a massive volume of spent garnet mixed with microscopic metal kerf. This sludge accumulates rapidly in the catcher tank. Manual removal involves shutting down the machine, draining the tank, and shoveling out the heavy, wet sludge. This is a labor-intensive process that causes significant machine downtime. Automated abrasive removal systems utilize sweeper packages or weir tanks. They continuously extract the sludge while the machine operates. Facilities must also establish protocols for drying and disposing of the spent material in accordance with local environmental regulations.
Foundation Assessment: Verify the concrete slab thickness and load-bearing capacity to support the water-filled catcher tank and heavy steel plates.
Electrical Infrastructure: Install dedicated high-amperage circuits with appropriate disconnects for the main pump motor and the CNC control console.
Water Quality Testing: Analyze the municipal water supply for Total Dissolved Solids (TDS) and hardness to determine if a reverse osmosis system or water softener is required.
Drainage and Waste Routing: Establish a clear path for overflow water drainage and designate a staging area for drying spent abrasive sludge before disposal.
Climate Control: Ensure the operating environment maintains stable humidity levels to prevent abrasive garnet from clumping inside the delivery hoppers.
To finalize your equipment selection and ensure a successful installation, execute the following steps:
Request custom test cuts from manufacturers using your specific material grades and thicknesses to verify edge quality and taper control firsthand.
Conduct a comprehensive site audit with a structural engineer to confirm your facility meets the foundation, electrical, and water quality requirements.
Calculate your projected hourly operating expenses based on local utility rates, abrasive garnet availability, and expected consumable wear.
Establish a dedicated waste management protocol for handling, drying, and disposing of the spent abrasive sludge generated during daily operations.
A: A commercial waterjet can effectively cut through steel up to 10 to 12 inches thick. As thickness increases, the cutting speed decreases significantly, and stream lag becomes more pronounced. Cutting materials beyond 6 inches usually requires specialized high-pressure pumps operating at 90,000 PSI and slower feed rates to maintain acceptable edge quality and dimensional accuracy.
A: Waterjets cut without heat, eliminating the Heat-Affected Zone, warping, and edge hardening. Lasers are faster on thin metals but struggle with thick or reflective materials. Plasma is fast and effective for thick steel but leaves a rough edge and heavy dross. Waterjets offer unmatched versatility and edge quality at the cost of slower cutting speeds.
A: Entry-level machines offer capable cutting performance but often utilize generic components and basic software. Premium brands invest in proprietary taper-compensation software, highly durable pump seals, and advanced motion control. Premium systems generally provide higher uptime, tighter tolerances, and better access to experienced service technicians and replacement parts.
A: Yes. You can configure the equipment to operate as an automatic CNC waterjet cutting machine for ceramics, glass, and stone. Operators must adjust the cutting parameters, specifically using low-pressure piercing techniques to prevent brittle materials from cracking during the initial stream penetration. Abrasive flow rates and feed speeds are also adjusted based on the material's hardness.
A: Most premium waterjets come with proprietary CAM software optimized for their specific cutting heads and pump dynamics. You can use standard CAD programs like AutoCAD, SolidWorks, or Fusion360 to design parts. You then export the files as DXF or STEP formats into the machine's nesting and toolpath generation software.
A: The jewel orifice typically lasts between 40 to 100 cutting hours, while diamond orifices can last over 500 hours. The tungsten carbide mixing tube generally lasts between 50 to 100 hours. This lifespan depends heavily on the abrasive garnet quality, water pressure, and the precision of the alignment between the orifice and the tube.